For most common soft materials, such as plastics, fiberglass, rubber, and veneer, using standard open-end pop rivets carries the risk of tearing through the material. Instead, you should choose blind rivets that are better suited for soft materials, including peel rivets, tri-fold rivets, or other types that create a larger support surface on the blind side.
Table of Contents
Why Standard Blind Rivets Fail in Soft Materials
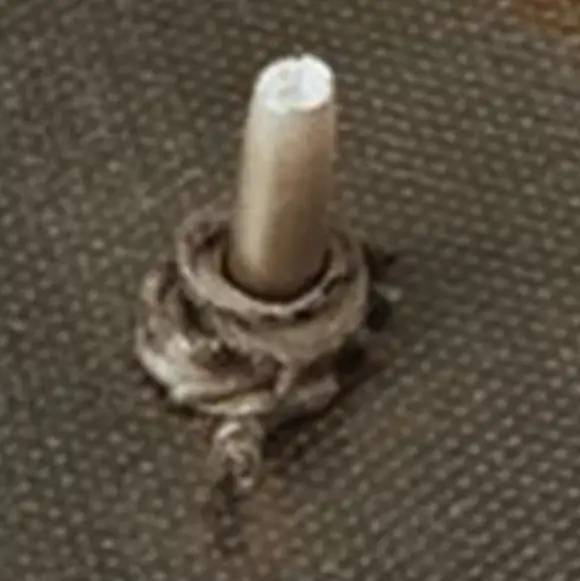
Standard open-end blind rivets are commonly used in materials such as thin metal sheets that possess a certain degree of hardness and load-bearing capacity. This is because during installation, the rivet exerts localized pressure on a small area of the sheet material. However, for materials such as plastic, fiberglass, rubber, cork, or other low-density materials, this concentrated pressure can exceed the material’s load-bearing capacity.
- If the deformed area on the blind side is too small, the material is prone to tearing through
In the riveting of Standard Blind Rivets, deformation must occur on the blind side to clamp the sheet metal. When the joint is pulled, the load is concentrated around the hole. For thinner, softer materials, this can easily cause the sheet metal to tear through or the joint to loosen. - Excessive clamping force from the rivet can crush the material
The installation tool generates axial clamping force when pulling the mandrel. If the installation force or clamping range is not suited for soft materials, issues such as surface indentations, bulging around the hole edges, and flattening of the interlayer may occur after installation. - Excessive stress concentration at the hole edges of soft materials can cause cracking
Standard blind rivets require the sheet metal to be secured, so they must expand as they pass through all the holes to be joined. The resulting pressure is concentrated on the hole walls and edges. Under prolonged stress, joints in soft materials will fail.
When selecting soft-material rivets, we conduct preliminary test riveting on sheet metal samples. We not only verify that the rivets have securely clamped the sheet metal but also inspect for fine cracks around the holes, check that the sheet surface is flat, and confirm that deformation on the blind side is within normal limits. This ensures the stability of the customer’s product assemblies. Our technical team subjects the sheet metal to vibration, repeated loading, and temperature changes to test the performance of the joints, ensuring the compatibility of the rivets with the sheet metal.
Compare the Best Rivet for Soft Materials
Peel-type blind rivets

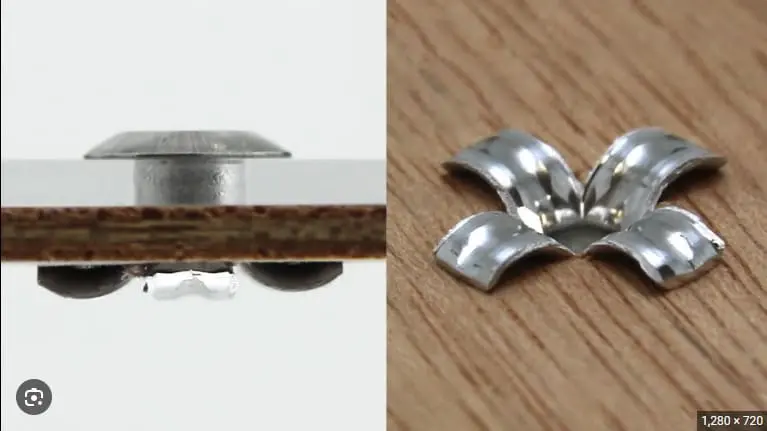
After installation, the tail end of a peel-type blind rivet forms multiple outward-spreading legs. This resembles the rivet “spreading its petals” on the back of the material. The multiple spreader legs distribute the localized pressure on the back side, dispersing the load around the hole and reducing the risk of the rivet sinking into the material or being pulled through the hole.
Peel-type blind rivets are particularly suitable for wood, rubber, plastic, laminates, and soft materials with uneven surfaces. Their primary advantages are load distribution and prevention of pull-through; they are not suitable for high-strength structural fastenings.
Tri-fold blind rivets
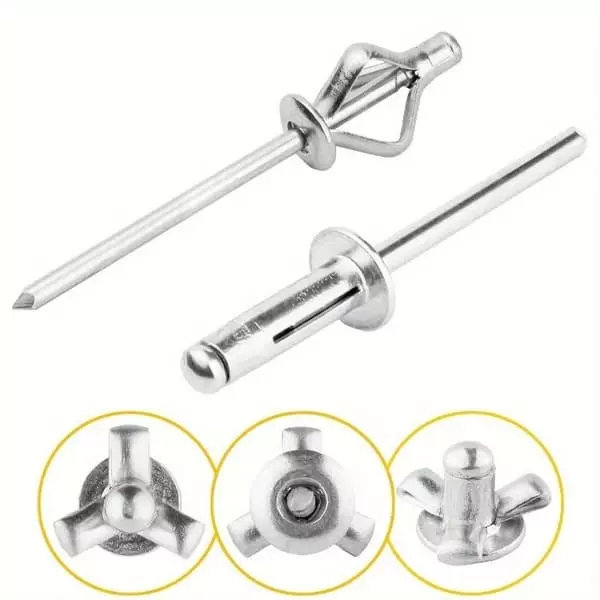
After installation, tri-fold blind rivets form three wide, folded legs on the blind side. They are particularly suitable for joints where soft material is located on the blind side, as these three legs evenly distribute the clamping force across the back of the material. For issues such as crushing, deformation, and tearing of soft materials, Tri-fold Blind Rivets are more suitable than standard open-type blind rivets.
Compared to Peel-type Blind Rivets, the Tri-fold type forms a wider and more uniform support area on the blind side. This is ideal for joints requiring more even load distribution.
Hem Firm Blind rivets
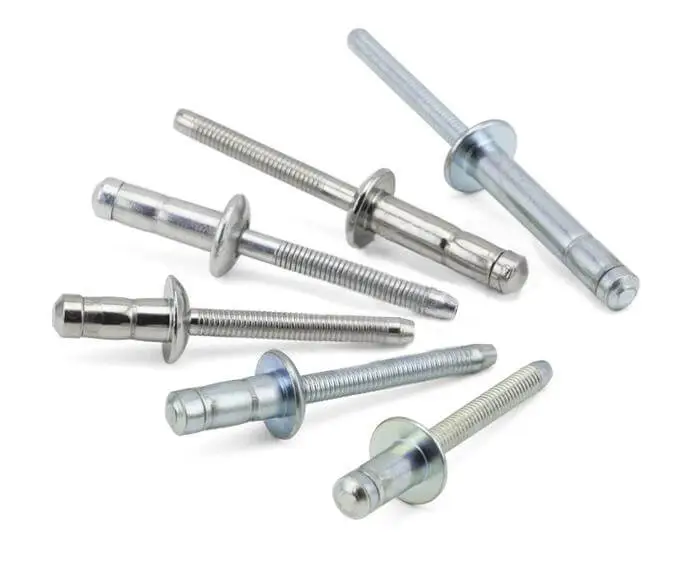
Hem-Firm is a high-strength structural blind rivet. After installation, it forms a large load-bearing tail on the blind side, and the resulting mandrel-locking structure enhances tensile, shear, and vibration resistance. It is particularly suitable for joints that require high connection strength, vibration stability, and mandrel retention capability.
For thinner or lower-strength materials where joints must withstand high loads or continuous vibration—such as connections in vehicle bodies, equipment housings, or transportation structures—you may want to consider Hem-Firm. Compared to Peel-type Blind Rivets and Tri-fold Blind Rivets, which focus on protecting soft materials, Hem-Firm emphasizes structural strength, a large load-bearing area on the blind side, and mandrel stability.
Large-flange blind rivets

Large-flange blind rivets increase the contact area on the front side, reducing the risk of the rivet head pressing into soft materials, causing dents, or tearing through the front surface.
The large-flange design is particularly effective when soft material is located on the side where the rivet gun is operated, and the blind side consists of harder materials such as steel or aluminum sheet.
When selecting blind rivets for soft materials on behalf of our customers, we do not consider only the strength of the rivet. The focus is first on determining whether the soft material is located on the face or the blind side of the joint, whether the material is prone to compression, and how much load the joint needs to withstand. The most common mistake made during the actual selection process is to consider only large-flange rivets when the soft material is on the blind side. However, while a large flange can only expand outward, it cannot increase the deformation zone on the blind side. Therefore, it is essential to also examine the shape of the back side after the rivet is installed to evaluate whether to use tri-fold blind rivets or peel-type blind rivets.
Select by Material: Plastic, Fiberglass, Wood, Rubber, Fabric
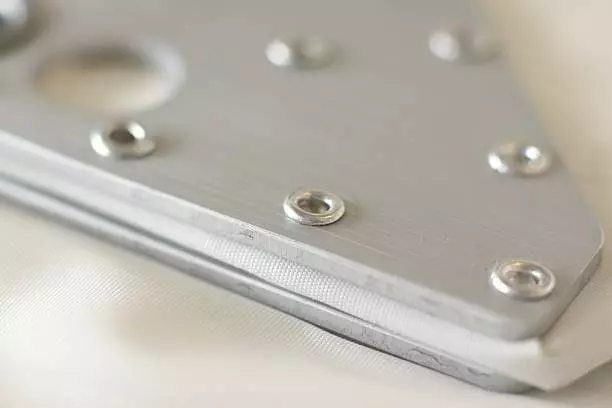
When selecting blind rivets for plastic, fiberglass, wood, rubber, or fabric, you cannot consider only the material. You need to determine whether the soft material is prone to cracking, compression, creep, or tearing, and whether it is located on the face or the blind side of the joint. You also need to consider material thickness, hole diameter, clamping range, rivet material, and installation load when making your selection.
| Material | Primary Failure Risks | Recommended Rivets to Test | Suitable Conditions | Important Considerations |
|---|---|---|---|---|
| Plastic | Cracking, indentation, creep and pull-through | Tri-fold, peel-type or large-flange blind rivets | Select according to the plastic’s stiffness and the position of the soft material | Brittle plastics should not be exposed to excessive installation loads |
| Fiberglass | Hole-edge cracking, delamination and pull-through | Tri-fold, peel-type or large-flange rivets with a backup washer | Non-structural housings, decorative panels and light-duty joints | Hole quality and blind-side bearing area are especially important |
| Wood | Wood-fiber crushing, hole enlargement and edge splitting | Peel-type or large-flange peel rivets | Plywood, softwood and light-duty wooden components | Screws or through-bolts are usually better for structural solid-wood joints |
| Rubber | Over-compression, creep and tearing around the hole | Large-flange rivets with backup washers or rigid support components | Applications where rubber acts as a sealing or cushioning layer | Do not rely on soft rubber alone to support the joint load |
| Fabric | Fiber tearing, hole enlargement and rivet pull-out | Large-flange rivets with backup washers or peel rivets with reinforcement | Multi-layer fabrics, conveyor belts and reinforced fabrics | Ordinary fabrics usually require washers, reinforcement patches or grommets |
Measure Grip Range and Choose Diameter
What Is the Grip Range of a Blind Rivet?
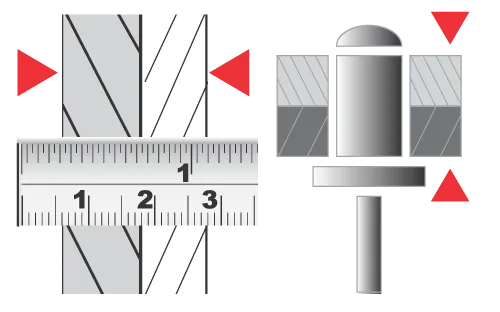
The grip range refers to the total thickness range of all materials to be joined that a blind rivet can properly grip.
- Formula for calculating the total joint thickness:
Total joint thickness T = Thickness of the first material layer + Thickness of the second material layer + Thickness of the washer + Thickness of other gripped layers - The selected rivet grip range must satisfy the following:
Minimum grip thickness ≤ Total joint thickness T ≤ Maximum grip thickness
How Should Compressible Materials Be Measured?
When materials are relatively hard—such as metal sheets and stiffer fiberglass—the thickness of each material layer can be measured directly using a vernier caliper. When the material is less rigid and prone to compression after riveting—such as rubber, foam, soft plastics, fabrics, and low-density wood—there is a difference between the total thickness before riveting and the actual thickness after installation.
Therefore, when the joint contains compressible materials, you must first determine the allowable compression thickness. You should measure the joint thickness based on the designed compression state, while also considering the use of stop sleeves, rigid shims, or support members to control the amount of compression.
How Do You Choose the Blind Rivet Diameter?
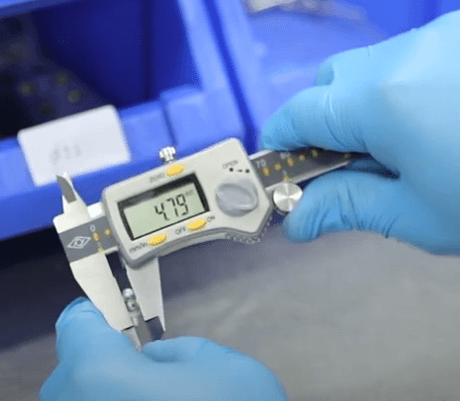
The blind rivet diameter refers to the outer diameter of the rivet body. Common sizes range from 3.2 to 6.4 millimeters. As the diameter increases, the rivet’s shear and tensile strength typically improve. However, the localized stress that the sheet material must withstand may also increase.
You can select the diameter by following these steps:
- Determine what type of load the joint will primarily bear: shear, tensile, peel, or vibration.
- Refer to the supplier’s technical data sheet for shear and tensile strength values based on the rivet type, body material, and mandrel material.
- Confirm the maximum load the area around the hole in soft materials can withstand to prevent the rivet’s strength from causing the material to tear through prematurely.
- Check whether there is sufficient edge clearance and rivet spacing at the drill hole location to prevent large-diameter holes from weakening the material.
- Perform test riveting on the actual material and inspect the hole edges, material surface, and blind-side forming condition.
In projects involving soft materials, we have found that quality issues with rivet installation are not due to incorrect rivet selection, but rather to a mismatch between the clamping range and the actual thickness of the joint. This results in the blind-side formation being too far from the sheet after installation, or the rivet body not being long enough to provide complete blind-side support. Therefore, before determining the rivet specifications, we need to verify the minimum and maximum thicknesses within the rivet’s clamping range and perform test riveting using both of these thicknesses.
Choose Head, Body, Mandrel, and Finish
Choose the Head Style
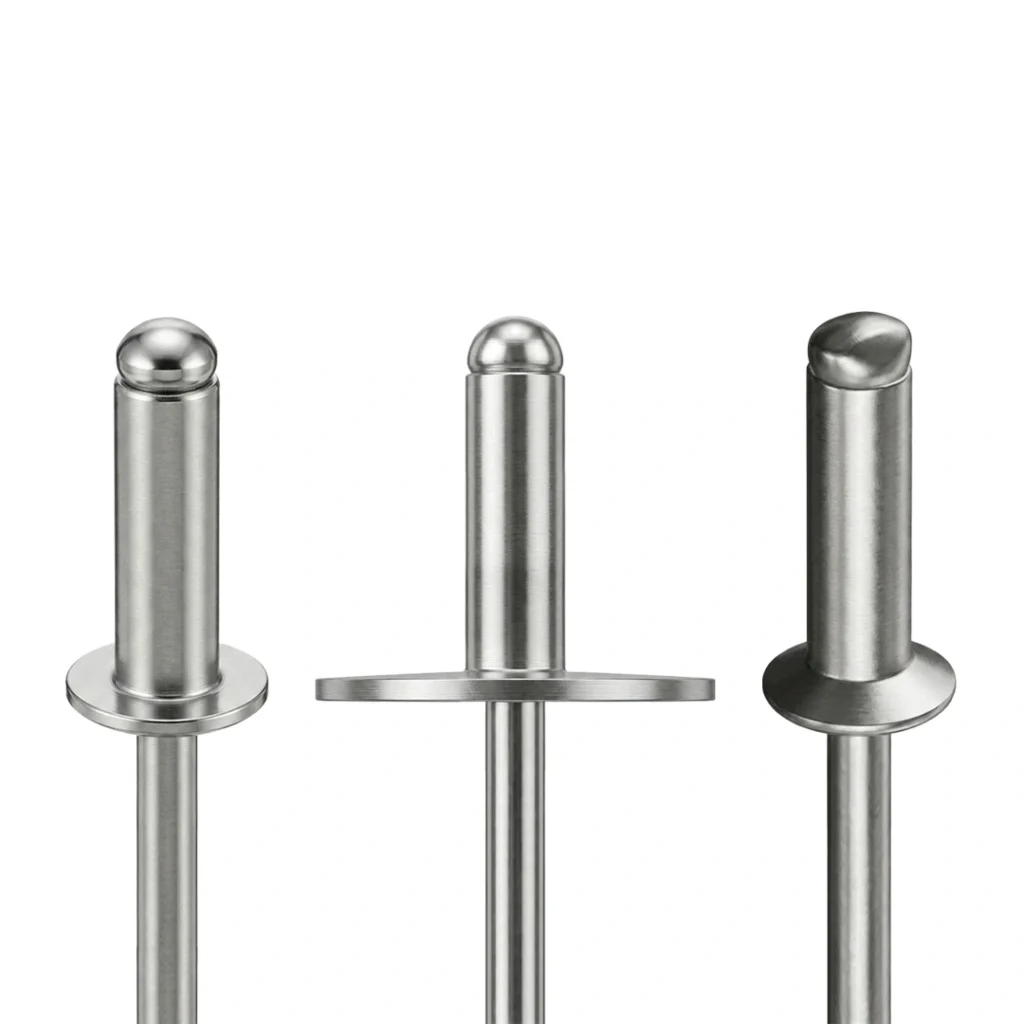
There are three common types of rivet heads: dome head, large flange head, and countersunk head. For soft materials, countersunk blind rivets are not recommended. Machining countersunk holes weakens the material around the hole edges, increasing the risk of cracking in plastic or fiberglass-reinforced plastic.
| Head Type | Main Features | Suitable Soft-Material Joints | Important Considerations |
|---|---|---|---|
| Standard Dome Head | Medium-sized head with good general-purpose versatility | Supported plastic panels, thicker fiberglass and light-duty joints | The front-side bearing area may be insufficient for very soft or thin materials |
| Large-Flange Head | Increases the front-side contact area and reduces localized pressure | Soft plastics, fiberglass, plywood, rubber layers and reinforced fabrics | It protects only the front side and cannot prevent blind-side pull-through by itself |
| Countersunk Head | Creates a flush or nearly flush finished surface | Materials with sufficient thickness and a correctly prepared countersunk hole | Countersinking reduces the effective material thickness around the hole and is generally unsuitable for thin, soft or brittle materials |
Choose the Rivet Body
The rivet body determines how the rivet deforms on the blind side. Standard open-end blind rivets form only a relatively concentrated bulge on the blind side. In contrast, peel-type and triple-fold rivets can form multiple legs, which distribute the load.
| Rivet Body Design | Blind-Side Shape After Setting | Suitable Applications | Main Limitations |
|---|---|---|---|
| Standard Open-End Rivet | Forms a relatively small and concentrated blind-side bulb | Light-duty joints where the material has adequate rigid support | More prone to pull-through in soft, thin, or low-density materials |
| Peel Rivet | Splits and expands into multiple petal-shaped legs | Wood, rubber, laminates, and applications with irregular blind-side surfaces | Generally not the first choice for high-load structural joints |
| Tri-Fold Rivet | Forms three wide folded legs on the blind side | Plastics, fiberglass, thin panels, and materials that deform easily | Requires sufficient clearance on the blind side for proper leg formation |
| Hem-Firm Rivet | Forms a larger blind-side bearing area while retaining the mandrel | Joints requiring higher tensile, shear, and vibration resistance | Higher setting loads may be involved, so suitability for soft materials should be verified by testing |
| Closed-End Rivet | The rivet body is closed at the blind end, helping reduce potential liquid or gas leakage paths | Enclosures and assemblies requiring improved water or dust resistance | A closed-end design does not automatically provide a larger blind-side bearing area |
| Body Material | Description |
|---|---|
| Aluminum | Lightweight, easier to deform during setting, and relatively lower in strength. Commonly used for plastics and light-duty applications. |
| Steel | Usually stronger than aluminum and suitable when higher mechanical strength is required. |
| Stainless Steel | Provides good strength and corrosion resistance. Often selected for outdoor, wet, or corrosive environments. |
| Aluminum Body + Steel Mandrel | A common combination that balances relatively easy setting with suitable mechanical performance for many general applications. |
Choose the Mandrel
During installation, the mandrel is pulled by the rivet gun, causing the rivet body to deform and eventually fracture once the design load is reached. The mandrel material, fracture load, and fastening method all affect the rivet’s installation load, blind-side forming, and vibration stability.
| Mandrel Type | Main Features | Suitable Applications | Important Considerations |
|---|---|---|---|
| Steel Mandrel | Provides good strength and forming capability and is widely used in blind rivet applications. | Aluminum-body peel rivets, tri-fold rivets and general industrial joints. | In wet or humid environments, consider the corrosion risk of any retained steel mandrel inside the rivet. |
| Aluminum Mandrel | Lightweight and offers good material compatibility, especially in all-aluminum rivet assemblies. | Light-duty joints, all-aluminum assemblies and some applications requiring improved corrosion compatibility. | Strength and forming capability are generally lower than those of a steel mandrel. |
| Stainless Steel Mandrel | Provides good corrosion resistance and relatively high strength. | Outdoor, wet and corrosive environments where improved durability is required. | Setting loads can be higher, so confirm that the rivet body can withstand the required installation load. |
| Locked-Mandrel Design | The mandrel is securely retained inside the rivet body after installation. | Joints exposed to vibration, higher loads or applications where reducing loose-mandrel noise is important. | Do not assume that a locked-mandrel design alone makes the rivet suitable for extremely soft materials. |
| Standard Break-Mandrel Design | Simple construction and generally lower cost. | General light-duty and non-critical fastening applications. | Check the mandrel break position and make sure the retained portion remains stable after installation. |
Choose the Finish
The right surface treatment can improve a rivet’s corrosion resistance and enhance its appearance. Before selecting a surface treatment, you should identify the rivet body, mandrel, the metals being joined, and the operating environment. If the materials being joined include aluminum sheet, steel sheet, or other metal support components, you must assess the risk of galvanic corrosion between different metals in a humid environment.
| Finish or Material Condition | Suitable Environment | Main Advantages | Important Considerations |
|---|---|---|---|
| Standard Zinc Plating | Indoor, dry environments with relatively low corrosion exposure | Cost-effective and commonly used for carbon steel blind rivets | Corrosion resistance can decrease if the zinc coating is damaged during handling or installation |
| Zinc-Nickel or High-Performance Protective Coating | Outdoor, humid, or more demanding corrosion environments | Generally provides better corrosion protection than standard zinc plating | Confirm the exact coating system and relevant corrosion test standard before specifying performance |
| Natural Aluminum or Treated Aluminum Alloy | Lightweight assemblies, general outdoor applications, and aluminum components | Low weight and good material compatibility with aluminum panels | For coastal or salt-spray environments, verify the specific aluminum alloy and surface treatment |
| Natural or Passivated Stainless Steel | Humid, outdoor, washdown, and corrosive environments | Provides inherent corrosion resistance without relying on a conventional plated coating | Stainless steel is not completely immune to corrosion; the grade must be matched to the actual service environment |
| Painted or Colored Coating | Applications requiring appearance matching, identification, or additional surface protection | Allows color matching while providing an additional protective surface layer | Coating thickness can affect rivet insertion, hole fit, and proper rivet setting |
Prepare the Hole and Install Without Damage
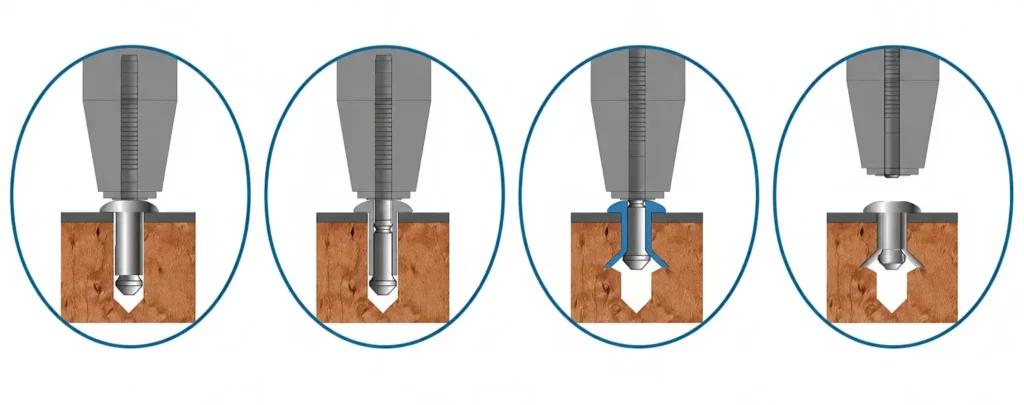
- Step 1: Confirm the rivet specifications: Check whether the diameter, grip range, head style, and body design are compatible with the sheet metal.
- Step 2: Confirm the recommended hole diameter: Follow the recommended hole diameter provided by the specific rivet manufacturer.
- Step 3: Drill the holes: Maintain a steady hand while drilling; you may use a soft material to provide back support.
- Step 4: Remove burrs: Remove any burrs or loose material that could interfere with the rivet’s fit.
- Step 5: Insert the rivet: Insert the rivet through all holes in the materials to be joined.
- Step 6: Press the workpiece firmly: Ensure the rivet head is in full contact with the workpiece surface.
- Step 7: Select the appropriate installation tool: The nozzle size, pulling force, and forming capacity must match the load-bearing capacity of the sheet metal.
- Step 8: Keep the tool vertical: Keep the nozzle, mandrel, and rivet axis as coaxial as possible.
- Step 9: Complete the riveting process.
- Step 10: Inspect the installed joint.
Common Failures and Fixes
| Failure Mode | What You May Observe | Common Causes | Priority Fix |
|---|---|---|---|
| Pull-Through | The rivet pulls through the material or the hole becomes enlarged | Insufficient bearing area, oversized hole, or material that is too thin or soft | Increase the front-side or blind-side bearing area |
| Cracking | Cracks appear around the rivet hole | Incorrect hole size, stress concentration, poor hole quality, or excessive installation load | Optimize the hole diameter, hole quality, and rivet design |
| Crushing | The material is visibly compressed, dented, or crushed | Localized clamping pressure is too high | Increase the bearing area and control the installation conditions |
| Loose Joint | The joint still has movement or clearance after riveting | Incorrect grip range, material rebound, or incomplete rivet formation | Check the total grip thickness and the final rivet formation |
| Head Sinking | The rivet head sinks into the surface of the soft material | Insufficient front-side bearing area | Use a large-flange rivet or add a suitable washer |
| Poor Blind-Side Formation | Peel or tri-fold legs do not form correctly | Incorrect grip range, insufficient blind-side clearance, or tool misalignment | Check the grip range, blind-side clearance, and installation setup |
| Hole Enlargement | The hole gradually becomes larger during service | Vibration, creep, cyclic loading, or micro-movement | Increase the bearing area and verify long-term load performance |
| Delamination | Fiberglass or laminated material separates around the hole | Drilling damage or excessive localized pressure | Improve hole preparation and blind-side load distribution |
FAQs
Does a larger rivet diameter always create a stronger joint in soft materials?
A larger rivet diameter does not necessarily result in a stronger bond with soft materials. This is because a larger diameter increases the rivet’s own tensile and shear strength. If the plastic or fiberglass is relatively thin and brittle, it is more prone to cracking, hole enlargement, or tearing through.
What is the difference between tri-fold rivets and peel rivets?
Tri-fold blind rivets and peel-type blind rivets differ in their forming methods and load distribution. After installation, tri-fold blind rivets form three relatively wide support legs on the back side. Peel-type blind rivets deform after riveting and spread outward into multiple petal-shaped support legs.
Can blind rivets be used in plastic?
Blind rivets can be used with plastic. The load-bearing capacity of the blind rivets you choose should be compatible with the strength and deformation capacity of the plastic itself.
Can stainless steel blind rivets be used in plastic and fiberglass?
Stainless steel pop rivets can be used with plastic and fiberglass-reinforced plastic . It is necessary to evaluate whether plastic and FRP can withstand the installation loads and localized stresses associated with stainless steel pop rivets.
Work with a IATF 16949 Certified Blind Rivet Manufacturer
Get High Quality Rivets Instead of Huck and Avdel Rivets
Rivmate Rivet
Rivmate is blind rivets manufacturers in china. The company is IATF 16949 certified and offers high-strength structural blind rivets that serve as alternatives to Huck and Avdel products.
Explore Rivmate Cases
Rivmate Rivet
Rivmate is blind rivets manufacturers in china. The company is IATF 16949 certified and offers high-strength structural blind rivets that serve as alternatives to Huck and Avdel products.
Hey There, I'm Allen!
I am the boss of Rivmate. For over two decades, we have specialized in the manufacture of blind rivets, providing our customers with reliable riveting solutions. Need riveting services? Feel free to contact us.