If you’re looking for blind rivets suitable for standard-thickness fiberglass, consider Tri Fold Rivets first.If the fiberglass is softer, we recommend using peel rivets. For connections requiring a tight seal, Bulb Tite rivets equipped with EPDM gaskets can be used.
When selecting the right pop rivets for fiberglass, consider the fiberglass thickness, connection load, operating environment, and installation conditions.
Table of Contents
Understand the Fiberglass Construction Before Choosing
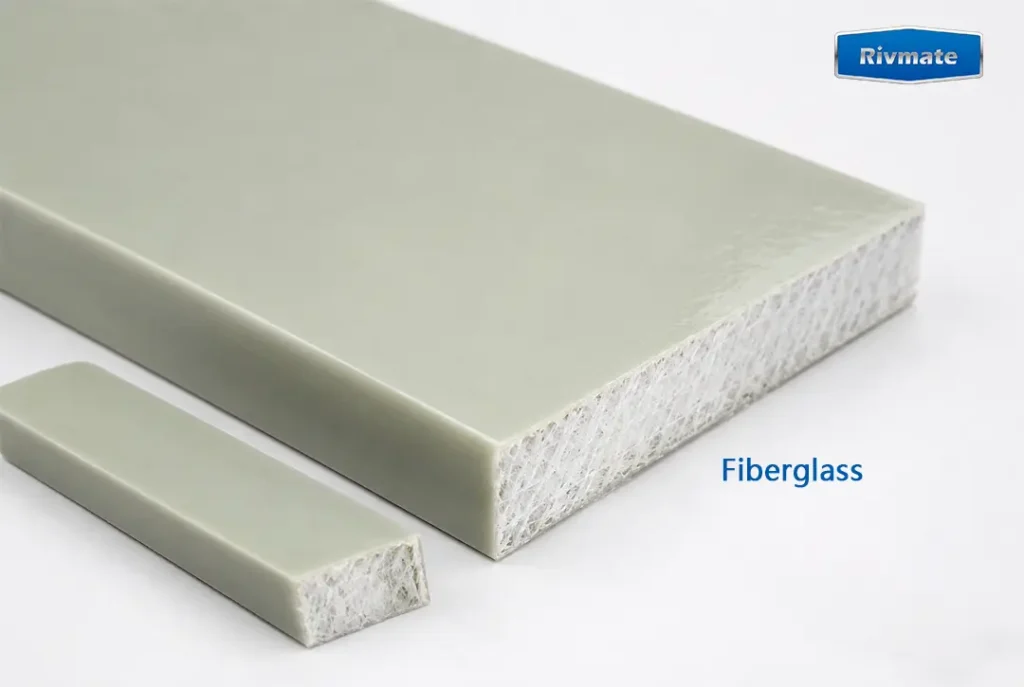
Fiberglass is a composite material made from a combination of glass fibers and resin. The glass fibers primarily provide strength and stiffness, while the resin holds the fibers in place and transfers loads. Different fiber orientations, resin types, molding processes, and internal structures of the panels result in fiberglass with varying load-bearing capacities.
Therefore, when selecting the appropriatepop rivets for fiberglass, you must clearly understand the internal structure of the FRP. Determine whether it is a solid laminate, a sandwich panel, a thin-walled molded part, or a structural FRP profile.
When addressing product selection for FRP projects, many of our customers provide only the total thickness of the sandwich panel without specifying that it contains a soft core material. If standard blind rivets are selected, installation will cause the internal core layer to be compressed, resulting in the rivet being secured only to the thin outer layer.
Why Standard Pop Rivets Crack or Pull Through Fiberglass
Compared to thin metal sheets, fiberglass-reinforced plastic (FRP) is at a higher risk of cracking and being torn through during rivet installation. This is because, during installation, the rivet relies on a small back-side locking head to clamp the sheet in place. The sheet must possess a certain degree of ductility and local load-bearing capacity. Due to its material structure, fiberglass cannot relieve local stress. As a result, it is prone to resin cracking, fiber-resin delamination, and interlaminar delamination.
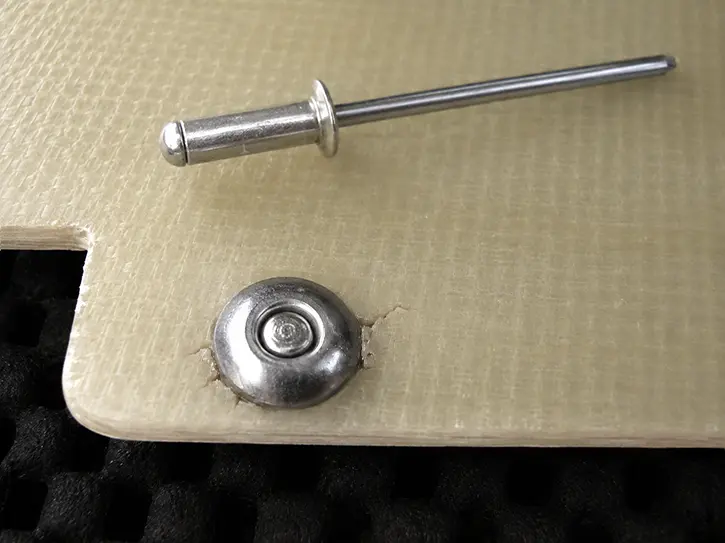
Installation pressure exceeds the local load-bearing capacity of the fiberglass-reinforced plastic (FRP): During installation, pop rivets require tensile force to deform the rivet body and clamp the panels together. Excessive tensile force can damage the edges of the FRP holes, posing a risk of internal resin cracks or delamination.
- Mismatched rivet clamping range: Selecting a clamping range that is too large or too small will result in uneven stress distribution on the rivet. This causes wear on the FRP hole walls, ultimately leading to loosening or the rivet pulling through the material.
- Excessively large drill hole diameter or poor drilling quality:After drilling FRP, issues such as chipped edges, burrs, exposed fibers, or localized delamination may occur. If the hole is drilled too large, the hole walls cannot be fully filled after riveting, resulting in a loose connection. If the hole is drilled too small, insertion will damage the hole walls and create microcracks that may expand over time.
- Vibrating environments can exacerbate existing damage: Vibration causes minute displacements between the fiberglass and the fasteners. Repeated vibration wears down the resin and fibers, gradually transforming round holes into oval ones.
When selecting rivets for thin-walled fiberglass equipment enclosures, we found that customers initially used standard aluminum pop rivets with wide flanges. Although the appearance appeared normal after installation, localized indentations still appeared on the back side. Upon inspection, we discovered that the wide flange only increased the load-bearing area on the front side, causing the pressure to concentrate on the locking head on the back side. By switching to triple-fold rivets, we were able to increase the load-bearing area on the back. For this type of FRP joint, increasing the load-bearing area on both the front and back is more effective than simply selecting standard pop rivets with higher strength.
Best Blind Rivet Types for Fiberglass
There are five common types of blind rivets suitable for fiberglass-reinforced plastic (FRP). Different types of rivets are suitable for different applications.
Peel rivets
After installation, the tail end of a peel rivet splits and flares outward, forming multiple petal-like legs. Compared to open-end pop rivets, they create a larger bearing surface on the back of the fiberglass-reinforced plastic (FRP). They are particularly suitable for thin FRP panels with low load-bearing capacity on the back that do not need to withstand significant tensile forces.

Tri-fold rivets
After installation, tri-fold rivets form three folded legs on the back of the fiberglass, distributing the clamping force over a larger area than standard locking heads. This effectively reduces the risk of hole-edge crushing and rivet pull-through. They also provide a wider clamping range, making them one of the most commonly used options for thin fiberglass. They are suitable for joining RV exteriors, fiberglass equipment enclosures, plastic-fiberglass composite assemblies, and vehicle interior and exterior panels or curved panels.
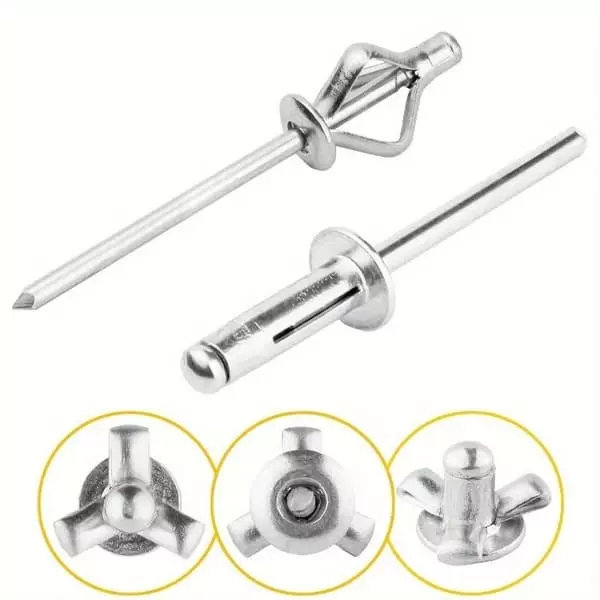
According to Rivmate’s current batch inspection data, the AAT48160 all-aluminum Tri-Firm rivet has dimensions of 4.8 x 16.0 mm, a nominal clamping range of 1.0–4.0 mm, and a recommended hole diameter of 5.0–5.2 mm. The report conducted installation inspections at both the upper and lower limits of the clamping range, as well as under two hole diameter conditions, testing five units per combination; all results were recorded as passing. This indicates that when selecting Tri-Firm rivets, one must not only verify the rivet diameter but also ensure that both the actual total thickness and the installation hole fall within the specified range for that model.
AAT48160 Tri-Firm Batch Inspection Table
| Inspection Item | Inspection Record / Result |
|---|---|
| Product | AAT48160, AL/AL Tri-Firm, 4.8 × 16.0 mm |
| Batch No. | 20230318 |
| Reported Quantity | 532,000 pcs |
| Grip Range Check | 1.0 mm and 4.0 mm |
| Test Hole Diameter | 5.0 mm and 5.2 mm |
| Test Samples | 5 pcs for each thickness / hole-diameter combination; report result: OK |
| Shear Test Result | 1,024–1,094 N; minimum specification: 750 N |
| Tensile Test Result | 1,345–1,492 N; minimum specification: 950 N |
| Mandrel Breaking Force | 1,790–1,840 N |
| Reference Standard | ISO 14589, applicable to the test items listed in the report |
The report uses steel shims or test fixtures, not FRP test panels. It can be used to demonstrate the performance of a product batch and to validate the clamping range.
Large-flange rivets plus a backing washer
The large-flange design increases the load-bearing area on the front face of the fiberglass. The washer on the back simultaneously increases the load-bearing area on the side of the locking head. Pressure on both the front and sides of the fiberglass is effectively dispersed, allowing the load to be distributed more evenly across both sides of the panel.
Plastic Tri-fold rivets
Once installed, plastic tri-fold rivets also form three support legs on the back. Their key advantages are that they are non-conductive, rust-resistant, and lightweight. The localized installation pressure is significantly lower than that of high-strength steel rivets. They are particularly suitable for securing electrical insulation covers, automotive interior trim, wiring harness brackets, lightweight decorative panels, or components where metal corrosion is undesirable.
Structural blind rivets

Structural blind rivets are used in fiberglass joints that must withstand high shear forces, tensile forces, impacts, or continuous vibration. These structural products feature a stronger rivet body, better hole-filling capability, and a locking mandrel, providing a more stable connection in vibrating environments.
In a comparative riveting test on fiberglass models, we found that when testing rivets of different designs—using rivets of the same diameter—triple-fold rivets, flower-head rivets, and standard pop rivets exert forces differently when forming on the back side of the fiberglass. This is particularly true for thinner fiberglass; rivets that form a larger supporting structure on the back side are more likely to achieve a stable connection.
When a Rivnut, Well Nut, Through-Bolt, or Bonded Fastener Is Better
| Connection Requirement | More Suitable Solution | Main Reason |
|---|---|---|
| One-Side Installation with Repeated Assembly and Disassembly | Rivnut / Rivet Nut | Creates a permanent internal thread in fiberglass and allows bolts to be installed and removed repeatedly. |
| Light Load, Vibration Isolation and Auxiliary Sealing | Well Nut | The rubber body expands during tightening, applies gentler pressure to the panel, and can provide vibration isolation and limited sealing. |
| High Load with Access to Both Sides | Through-Bolt | Uses a bolt, nut and often large washers or backing plates to distribute the load over a larger area. |
| Very Thin or Irregularly Shaped Fiberglass | Bonded Fastener | A larger bonded base distributes the load without creating significant local expansion pressure in the laminate. |
| Permanent, Fast, Light-to-Medium Load Connection | Pop Rivet / Blind Rivet | Fast one-side installation makes it suitable for efficient batch assembly where repeated disassembly is not required. |
Choose Grip Range, Diameter, Head, and Material
Step 1. Measure the total thickness of all parts to be joined and select the grip range
You need to measure the total thickness of the fiberglass-reinforced plastic (FRP), metal brackets, plastic fittings, and other rigid parts to be clamped. Since the thickness of some FRP structures may change after riveting, you must factor in sheet material tolerances, adhesive layers, and variations in part thickness. The clamping range must cover the actual thickness after riveting.
Batch inspections for the AAT48160 cover both the 1.0 mm and 4.0 mm clamping thicknesses at both ends, rather than just a test fit at the midpoint thickness. The main reason for this is that the same model may exhibit different back-side forming characteristics at the lower and upper limits of the clamping range. If your combination of FRP, metal brackets, sealing layers, or gaskets is close to the range limits, you should perform a test fit using the actual material combination; do not place an order based solely on the nominal plate thickness.
Step 2. Select the Diameter by Evaluating Joint Loads and FRP Compressive Strength
When selecting the diameter, you need to check two critical factors simultaneously: whether the rivet’s tensile and shear strengths can meet the joint loads, and whether the edges of the FRP hole can withstand the pressure transmitted by the rivet without crushing or tearing through.
In the AAT48160 batch report, when the 4.8 mm Tri-Firm was tested using a 5.2 mm test hole, the ISO 14589 shear test results ranged from 1,024 to 1,094 N, and the tensile test results ranged from 1,345 to 1,492 N, exceeding the minimum requirements of 750 N and 950 N listed in the report for this model. However, these results were obtained using steel test fixtures and reflect the performance of the rivet itself under specified test conditions; they cannot be directly used as the design allowable load for FRP joints. FRP joints still require verification based on hole-edge bearing capacity, interlaminar strength, and the actual installation structure.
Step 3. Select the Head Type Based on Load Distribution and Surface Requirements
The edge bearing capacity of FRP holes is lower than that of thin metal sheets. The larger flange of a Large Flange Head design distributes the clamping force from the front over a larger area, reducing the risk of the rivet head pressing into the FRP hole edge and causing cracking. When the FRP is prone to being pulled through from the back, you should select a tri-fold or peel rivet . You may also consider adding a back washer if access to the back of the FRP is possible.
| Head Type | Suitable Applications | Key Considerations for Fiberglass |
|---|---|---|
| Large Flange Head | Thin panels, brittle panels, or applications with relatively low edge-bearing strength | Preferred when you need to distribute the bearing pressure over a larger surface area. |
| Dome Head / Standard Flange | Thicker, more stable solid fiberglass panels and general-load applications | Make sure the flange does not apply excessive localized pressure to the panel surface. |
| Countersunk Head | Applications that require a flush or nearly flush surface | Countersinking removes laminate material, so it should be used carefully in fiberglass. |
| Sealed Head Type | RVs, boats, and outdoor equipment | A sealing washer or additional sealant may still be required when reliable water resistance is needed. |
Step 4. Select rivet body and mandrel materials based on the operating environment and corrosion resistance requirements
Pop rivets consist of two parts: the rivet body and the mandrel. The rivet body comes into direct contact with the fiberglass and forms a locking structure on the back side, while the mandrel is responsible for pulling and compressing the rivet body. You need to confirm the complete rivet body and mandrel combination based on the actual connection of the product.
| Material Combination | Main Characteristics | Best-Suited Fiberglass Applications |
|---|---|---|
| Aluminum Body / Aluminum Mandrel | Lightweight, corrosion-resistant, and relatively gentle during setting. | Thin fiberglass panels and light-to-medium load applications. |
| Aluminum Body / Steel Mandrel | Higher mandrel strength with a wide range of product options. | General industrial joints, provided installation force and corrosion are checked. |
| Stainless Steel Body / Stainless Steel Mandrel | High strength and strong corrosion resistance. | Thicker fiberglass panels, higher-load joints, and corrosive environments. |
| Nylon or Plastic Construction | Non-conductive, rust-free, and gentler on the panel. | Electrical enclosures, interior trim, and other light-load connections. |
Prepare the Hole Without Damaging the Laminate
The quality of mounting holes drilled in fiberglass-reinforced plastic (FRP) affects the connection performance after the rivets are installed. If the drilling method is incorrect, the hole edges may chip, the fibers may tear, the surface may turn white, or delamination may occur. Even minor damage can be magnified by the pressure and vibration during the riveting process. Therefore, it is important to machine mounting holes that are the correct size, have intact edges, and are perpendicular to the panel surface.
1. Confirm the hole diameter that matches the rivet
You should determine the hole diameter based on the manufacturer’s data sheet. The hole diameter should allow the rivet to be inserted smoothly without noticeable lateral play.
The product catalog and batch inspection data show that different Tri-Firm diameters correspond to different recommended hole diameters. For example, the 4.8 mm AAT series uses a 5.0–5.2 mm hole diameter, while the 5.2 mm Bulbtight Tri-Firm catalog specifies 5.3–5.5 mm. The rule of “0.1–0.2 mm larger than the rivet” should not be used as a blanket substitute for product specifications, as the recommended clearances vary depending on the specific structure and model. Before machining, verify the specific part number and drill holes according to the hole diameter requirements for that model.
2. Use a sharp drill bit suitable for fiberglass-reinforced plastic
Fiberglass is highly abrasive and can cause rapid wear on drill bits. Consider using a more wear-resistant drill bit designed for FRP or composite materials, and check the cutting edges regularly.
3. Secure the workpiece and support the back of the drill hole
Before drilling, secure the fiberglass panel to prevent it from moving when the drill bit makes contact. If access to the back is possible, place a shim there. Avoid letting the drill bit penetrate through the fiberglass to minimize chipping and fiber tearing at the exit point.
4. Keep the drill bit perpendicular to the panel surface
The drilling tool must be held perpendicular to the fiberglass surface, and a steady, continuous feed force should be applied. This minimizes heat generated by sustained friction, which can damage the resin at the hole edges.
5. Lightly clean the hole edges
Loose fibers, dust, and burrs will form after drilling, and you need to clean them up promptly. Ensure the rivet head sits flush against the panel without any gaps.
6. Check the hole opening for damage
Before installing the rivet, you should inspect the front, back, and walls of the hole for signs of damage:
- White ring-shaped marks around the hole opening;
- Fine cracks or notches in the gel coat
- Fiber tears or delamination on the back
- The hole diameter is noticeably too large or oval-shaped
- Loose fibers on the hole walls
- The rivet is noticeably tilted or wobbles after insertion
If any of the above issues are found, repair or rework the installation hole promptly using the correct method.
7. Consider Sealing the Hole Walls in Humid Environments
Drilling cuts through some of the fiberglass in the FRP, exposing the resin and fibers inside the hole walls. For FRP parts used outdoors, on boats, or in humid or chemical environments, the edges of the drilled holes must be sealed.
Rivmate’s Tri-Firm waterproofing comparison data documents a test conducted at a water column of 1 meter for 30 minutes. Among the samples shown in the report, the water level on the Rivmate side remained stable after the test, while the comparison samples showed a significant drop. The data also shows the EPDM gasket, the core rod groove, and the cross-section after riveting. However, the report does not specify the FRP substrate or the number of samples; therefore, while it demonstrates that the product’s structure has undergone waterproof testing, it cannot replace your own full-system waterproof verification conducted under actual FRP panel, hole wall, and sealant conditions.
Step-by-Step Pop Rivet Installation in Fiberglass
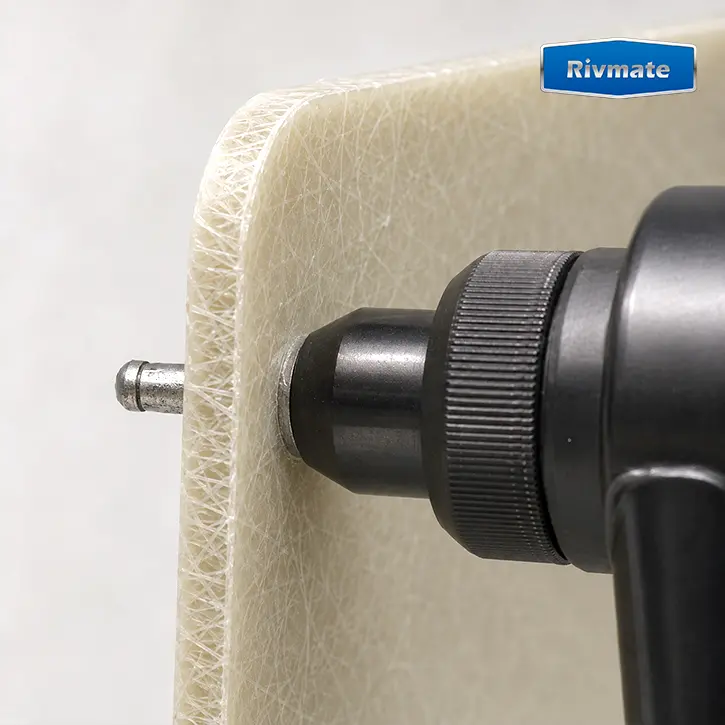
- Step 1: Determine the loads on the internal structure and connection points of the fiberglass-reinforced plastic.
- Step 2: Verify rivet specifications: Before installation, first confirm that the selected rivets are suitable for the joint in question.
- Step 3: Mark and align hole positions: Mark the riveting locations on the workpiece and ensure that the holes in all materials to be joined are precisely aligned.
- Step 4: Drill the Correct Hole Diameter: The size of the mounting holes must comply with the requirements specified in the specific rivet’s data sheet.
- Step 5: Remove Burrs.
- Step 6: Install Washers or Sealing Material as Required by the Product.
- Step 7: Fully Insert the Rivet: Ensure the rivet head is flush with the FRP surface.
- Step 8: Select the correct riveting tool and rivet head: The riveting tool must be compatible with the rivet’s diameter, mandrel size, material, and structure.
- Step 9: Hold the riveting tool vertically and pull the rivet steadily.
- Step 10: Break off the mandrel.
- Step 11: Inspect the installed rivets.
Application Selection Table
| Fiberglass Application | Preferred Fastening Solution | Why It Is Suitable | Key Considerations |
|---|---|---|---|
| Thin Solid Fiberglass Panels, No Backside Access, Light-to-Medium Loads | Aluminum Tri-Fold Rivet or Wide-Back Load-Spreading Blind Rivet | Creates a larger bearing area on the blind side after installation, helping distribute the load and reduce pull-through risk. | Check that the tri-fold legs expand completely and make sure the supported grip range matches the total material thickness. |
| Soft, Thin-Wall or Low Edge-Bearing Fiberglass | Peel Rivet | The rivet body separates into multiple legs on the blind side, distributing the load over a larger area. | Better suited to light-duty connections. High loads, severe vibration, or critical structural joints require separate validation. |
| Weak Fiberglass on Both Sides with Access to the Backside | Large Flange Blind Rivet + Backing Washer | The large flange distributes pressure on the front surface, while the backing washer spreads the rivet load on the blind side, protecting both surfaces. | The washer inner and outer diameters must be appropriate and must not interfere with normal rivet deformation. |
| Signs, Decorative Panels, Electrical Insulation Parts and Other Light-Load Components | Plastic Tri-Fold Rivet or Nylon Rivet | Requires relatively low setting force and provides electrical insulation and corrosion resistance. | Not recommended for primary structural loads, high-temperature service, or continuously vibrating joints. |
| Thicker, High-Quality Solid Fiberglass Laminates with Light Loads | Standard Dome Head or Large Flange Blind Rivet, After Sample Validation | Thicker laminates generally provide better bearing strength around the hole, so a standard blind rivet may be suitable. | Do not select the rivet only because the panel is thick. Still check the blind-side deformation size and inspect the laminate for edge cracking. |
| Medium-to-High Loads or Continuously Vibrating Joints with Backside Access | Structural Blind Rivet with Large Blind-Side Bearing Area and Mandrel Retention | Provides greater blind-side support and helps reduce the risk of a retained mandrel becoming loose during service. | Setting force may be higher, so verify that the fiberglass does not crack or become damaged during installation. |
| Fiberglass Access Covers Requiring Periodic Removal | Well Nut, Suitable Rivet Nut, Bonded Threaded Fastener or Through-Bolt | Provides a reusable threaded connection, avoiding the need to remove and replace a blind rivet every time the panel is opened. | Standard rivet nuts should not be used directly in thin fiberglass without validation. Check spin resistance, bearing area and installation pressure. |
| Foam-Core, Honeycomb-Core or Other Fiberglass Sandwich Panels | Local Reinforcement, Crush-Resistant Sleeve, Bonded Fastener or Load-Spreading Through-Bolt | Helps prevent the fastening force from directly compressing or crushing the soft core material. | Do not choose a longer rivet only according to the total panel thickness. The core’s resistance to compression is more important. |
| Outdoor, Marine, Humid or Water-Resistant Enclosures | Sealed Closed-End Blind Rivet or Validated Rivet + Sealing Material Combination | Allows both blind-side load distribution and sealing around the installation hole to be considered. | A “closed-end” rivet does not automatically make the complete joint waterproof. Also check sealing under the head, around the hole wall and at all fit gaps. |
Common Problems and Fixes
The installation quality of FRP pop rivets depends not only on the rivets themselves but is also influenced by the FRP laminate structure, installation holes, grip range, riveting tools, and installation methods.
Common issues encountered during the installation of FRP pop rivets include protruding rivet heads, sunken rivet heads, loose joints, panel cracking, and abnormal breakage of the rivet shank. Should any of these problems arise, a specialized inspection must be conducted immediately to resolve them.
| Common Problem | Possible Cause | Corrective Action | What Not to Do |
|---|---|---|---|
| Whitening or Cracks Around the Rivet Head | The hole edge was already damaged during drilling; setting load is too concentrated; the rivet body is too hard; or the edge distance is insufficient. | Inspect the hole edge and blind-side formation. Consider a rivet with a wider blind-side bearing area and improve the drilling process. Repair the fiberglass first if the damage is severe. | Do not simply use a larger rivet head to cover the crack and continue using the joint. |
| Rivet Pulls Through the Fiberglass | The blind-side bearing area is too small; the fiberglass is too thin; the hole is oversized; or the actual load exceeds the panel’s local bearing capacity. | Evaluate tri-fold, peel-type, or wide blind-side rivets. Add a load-spreading washer when backside access is available. For higher loads, consider a backing plate or through-bolt. | Do not solve the problem only by replacing the rivet with a higher-strength steel rivet. |
| Rivet Remains Loose After Installation | Incorrect grip range, oversized hole, gaps between components, or incomplete blind-side deformation. | Re-measure the total material thickness, check the hole diameter, clamp the components together before riveting, and use a rivet with the correct grip range. | Do not hammer the rivet head or attempt to pull the mandrel again after it has already broken. |
| Rivet Head Does Not Sit Flat on the Panel | The installation tool is tilted, the fiberglass surface is curved, dust remains inside the hole, or the mating component is warped. | Clean the installation hole, align the components with a fixture, and keep the riveting tool aligned with the rivet axis. | Do not force the rivet head flat with the tool or hammer it against the fiberglass. |
| Blind-Side Rivet Deformation Is Biased to One Side | Misaligned holes, an angled installation tool, an irregular hole, or a washer interfering with rivet expansion. | Check hole alignment, tool angle, and available blind-side space. Prepare another sample and confirm that the rivet forms symmetrically. | Do not judge installation quality only from the appearance of the front side. |
| Mandrel Breaks Too Early | Rivet deformation is obstructed; the grip range is incorrect; the tool, nosepiece, or rivet is mismatched; or the tool jaws are worn. | Stop installation and verify the complete rivet specification. Check tool capacity, nosepiece compatibility, and installation hole dimensions. | Do not simply increase the tool pressure and continue installation. |
| Mandrel Is Difficult to Break | The rivet material or diameter exceeds the tool capacity; tool stroke or gripping capability is insufficient; or the wrong nosepiece is being used. | Use the manufacturer-approved installation tool and nosepiece, and check the maintenance condition of the tool. | Do not repeatedly bend the mandrel from side to side or forcibly twist it off with pliers. |
| Visible Depression in the Fiberglass Surface | Local clamping force is too high, sandwich-panel core material is being compressed, or assembly gaps exist between the components. | Use a wider load-spreading structure. For sandwich panels, consider a compression-resistant sleeve, local potting, or reinforcement plate. Remove assembly gaps before installation. | Do not continue using the same rivet and assume that reducing installation speed will solve the problem. |
| Joint Becomes Loose Again After a Period of Use | Continuous vibration, repeated fiberglass panel flexing, fatigue damage around the hole, or an inadequately retained mandrel. | Inspect the fiberglass around the hole and the overall structural stiffness. Evaluate a mandrel-retaining structural blind rivet, add support, or reposition the fastening points. | Do not install another rivet of the same size directly into the already damaged hole. |
| Water Ingress or Corrosion in Outdoor Joints | An open-end rivet was used, the hole is oversized, the area under the rivet head is not sealed, or the rivet material is incompatible with the metal support structure. | Select an appropriate sealed or closed-end rivet and compatible material combination. Seal the hole wall and area beneath the rivet head as required, then perform an actual water-ingress or sealing test. | Do not assume that using a closed-end rivet automatically makes the entire joint waterproof. |
Get a Fiberglass Rivet Recommendation
If you’re still unsure which type of pop rivets to choose for fiberglass, you can send the following information to Rivmate:
- Fiberglass structure and thickness
- Total thickness of the actual joint
- Current installation hole dimensions
- Loads, vibration, and operating environment
- Product photos, drawings, or samples
- Number of test samples and estimated purchase quantity
As one of China’s top three blind rivet manufacturers, Rivmate specializes in providing high-volume supply and customized pop rivet solutions to customers worldwide. Our professional team will recommend the most suitable pop rivets based on your product requirements and assembly environment.
FAQs
Can You Use Pop Rivets in Fiberglass Sandwich Panels?
Blind rivets can be used on fiberglass-reinforced plastic (FRP) sandwich panels. FRP sandwich panels primarily consist of two thin FRP facings with a foam, honeycomb, or other lightweight core material in between. Therefore, when installing with standard blind rivets, localized physical reinforcement must be applied to the FRP sandwich panel.
How Close Can a Pop Rivet Be to the Edge of Fiberglass?
There is no single minimum edge clearance that applies to all panels. You need to determine the appropriate clearance based on the fiberglass thickness, fiber layup, rivet diameter, load direction, hole edge quality, and the method used to form the back surface.
Can Pop Rivets Be Used for Structural Fiberglass Joints?
Pop rivets can be used to join fiberglass-reinforced plastic (FRP) structures. Standard pop rivets cannot be used for load-bearing connections in FRP structures.
It is important to distinguish between “catalog tensile/shear values for rivets” and “allowable loads for FRP joints.” The former are typically derived from standard fixture tests, while the latter are also influenced by the FRP layup, resin system, distance from the hole edges, hole machining quality, back-side formed area, load direction, and environmental factors. Therefore, even if the rivet itself meets the catalog performance specifications, critical FRP load-bearing joints cannot be directly approved based on this alone. For critical structures, joint-level testing should be conducted using the actual materials and hole location
Work with a IATF 16949 Certified Blind Rivet Manufacturer
Get High Quality Rivets Instead of Huck and Avdel Rivets
Rivmate Rivet
Rivmate is blind rivets manufacturers in china. The company is IATF 16949 certified and offers high-strength structural blind rivets that serve as alternatives to Huck and Avdel products.
Explore Rivmate Cases
Rivmate Rivet
Rivmate is blind rivets manufacturers in china. The company is IATF 16949 certified and offers high-strength structural blind rivets that serve as alternatives to Huck and Avdel products.
Hey There, I'm Allen!
I am the boss of Rivmate. For over two decades, we have specialized in the manufacture of blind rivets, providing our customers with reliable riveting solutions. Need riveting services? Feel free to contact us.